Solution stories
Corrugated Packaging: Job Costing and Machine Utilisation
Job-level costing, board planning and setup reduction for a box maker.
 Trikaan Research & Engineering4 min read
KEY TAKEAWAYS
- Every order is a different size, ply and print — costing by average loses money.
- Board planning across orders reduced trim waste.
- Corrugator and printer OEE revealed setup losses.
- Actual cost per job changed pricing conversations.
A corrugated box maker with many small orders found that some customers were unprofitable but could not prove which.
This story shows how job-level data changed decisions.
The situation
Costing used average rates per box type. Corrugator schedules were planned manually. Setup times on printers were not recorded.
What they had already tried
- Price increases across the board.
- Manual trim calculations.
- More shifts on the printer.
How we diagnosed the real problem
We captured job-level data for a month.
- Small runs with complex prints were heavily under-costed.
- Trim waste varied with deckle planning.
- Setups consumed a large share of printer time.
The solution, product by product
No single product solved this. The value came from the products working on the same data.
| Product | Role in this solution |
|---|---|
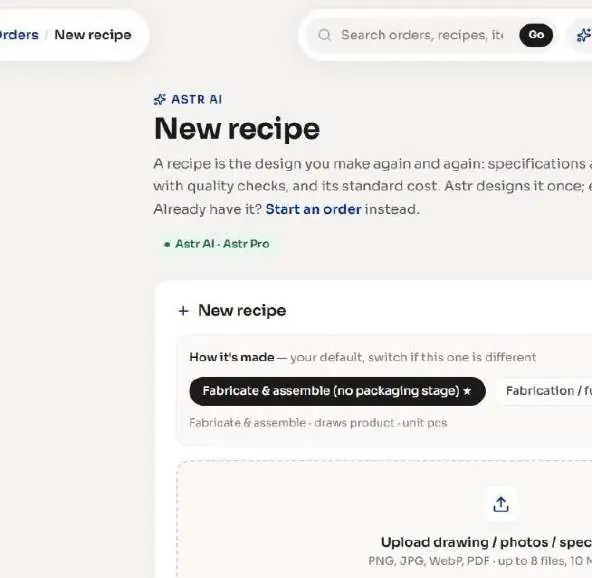
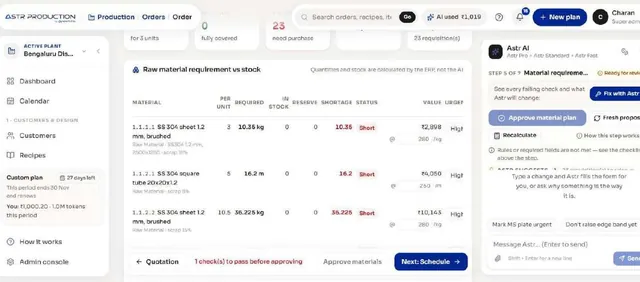
| ASTR Production | Job specs, board planning and deckle optimisation, actual cost per job |
| Machine Digital Twin | Corrugator and printer run, setup and stop times |
| Anvaya | Paper reels, stock, purchase, dispatch, invoicing |
| ASTR Reporting | Margin by customer, job size and print complexity |
How it rolled out
- Job-level capture.
- Board planning.
- Machine monitoring.
- Margin reviews with sales.
What changed
Pricing became job-specific and capacity was recovered from setups.
- Trim waste reduced by [X]%.
- Printer setup time reduced by [X]%.
- Unprofitable customer segments identified and repriced.
What we would tell a similar company
- Cost every job individually.
- Plan board across orders.
- Measure setups.
- Share margin data with sales.
Frequently asked questions
Can it optimise deckle?
Board planning groups orders to reduce trim.
Do we need machine sensors?
Run and stop signals improve accuracy; manual capture is a start.
Is this a real customer?
It is an illustrative composite.
- #packaging manufacturing software case study
- #corrugated box costing
- #packaging job costing
- #corrugator OEE
- #box plant ERP
Trikaan Research & Engineering
Trikaan
Written by the researchers and engineers who build Anvaya, ASTR and Seed Track, with input from Trikaan's delivery and engineering teams.